Screws & barrels for extruders
Nitrided, hard-chrome and bimetallic screws and barrels from 25 to 150 mm, made in Sai Extrumech's dedicated screw and barrel unit in Faridabad, for new extruders, replacements and repairs.
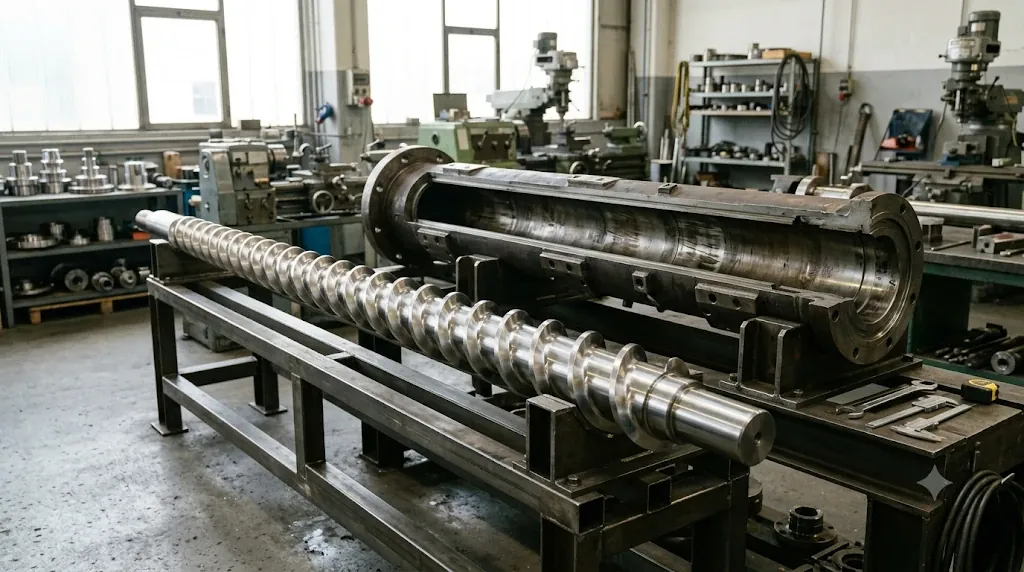
An extruder screw with its barrel opened for inspection.
Range
| Diameter | 25 mm to 150 mm |
|---|---|
| L/D ratio | 20:1 to 32:1 |
| Screw finishes | Nitrided; hard chrome (950 HV and above); bimetallic hard-facing (55–72 HRC) |
| Surface finish | Ra 0.4 µm on screw flights |
| Barrels | Nitrided or bimetallic-lined |
| Flight geometry | Matched to the compound: PVC, PE, XLPE, HFFR/LSZH and others |
Nitrided or bimetallic?
Nitrided sets have a hardened case on the steel itself. They are the cost-effective choice for unfilled PVC and PE, which do little abrasive work.
Bimetallic barrels have a separate hard alloy lining bonded inside the barrel, and bimetallic screws carry a hard-facing on the flights. There is far more wear material, so they last longer on abrasive and filled compounds: filled XLPE, HFFR/LSZH, glass and mineral-filled materials. A full comparison is in this article on nitrided vs bimetallic screws and barrels.
Choosing the right screw
Material is only part of the order. The L/D ratio, compression ratio and flight depths have to suit the compound: a PVC screw can over-shear HFFR, and a long screw can scorch silane XLPE. Tell us the compound, the output you need in kg/h and your extruder, and we will recommend the geometry.
Replacements and repair
- Replacement sets for extruders from other makers, made from the old parts, a drawing or measured dimensions.
- Screw repair: worn flights rebuilt and re-hardened, often for much less than a new screw.
- Measure both parts first. Output depends on the clearance between screw and barrel, so a new screw in a badly worn barrel will not restore it.
Signs of screw and barrel wear
- Output in kg/h falling at the same screw speed.
- Surging: melt pressure and cable diameter pulsing.
- Rising melt temperature, or more scorch and black specks.
- Unmelted particles reaching the die.
For prevention, see the guide on stopping screw and barrel wear.
Ask for a screw and barrel quotation
Send the extruder make and size, the compound with filler type and percentage, your target output, and a drawing or photo of the old set if it is a replacement.
Frequently asked questions
Which is better, a nitrided or a bimetallic screw and barrel?
Nitrided sets are cost-effective for unfilled PVC and PE. Bimetallic barrels have a hard alloy lining and last longer with abrasive, filled or flame-retardant compounds such as HFFR and filled XLPE. Choose by the compound you run.
What sizes of screw and barrel do you make?
Screw and barrel sets from 25 mm to 150 mm diameter, with L/D ratios from 20:1 to 32:1, and flight geometry matched to the compound.
Can you make a replacement screw and barrel for another make of extruder?
Yes. Replacement screws and barrels can be made for extruders from other makers using the old parts, a drawing or measured dimensions.
Can a worn screw be repaired?
Often yes. Worn flights can be rebuilt and re-hardened, which costs less than a new screw. Whether repair makes sense depends on the wear and the state of the barrel, so both should be measured first.